
Summary
More Industry Related Content
With Andrew Stock
What was the problem on site and why was it repeatedly happening?
Wash is the fermented liquid which actually serves as the base for the distillation. A grain distillery column’s stills are a constant process, the wash is being pumped in constantly unless down for maintenance. A band aid approach was being taken, repair as quick as possible and keep the process running.
It looks as if the company was having multiple difficulties? Were they unaware of them or was it a case of worrying about the cost of replacing their system?
The awareness and the size of the problem came to light on a maintenance review.
Was the problem obvious to you on first sight and was it an easy fix?
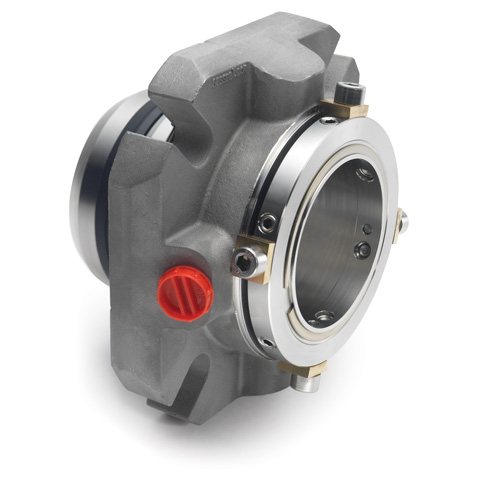
Fifteen years’ experience tends to give you an insight on how to see a fix on equipment like this. Wash is hot and sticky, nitric is corrosive and used often to remove scale from systems. Caustic dissolves mineral deposits. Each liquid requires respecting when pumping and sealing. Using good, reliable technology to seal them.
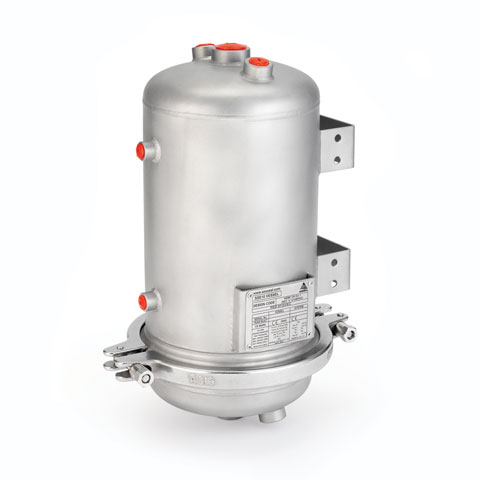
Why was the EasyClean™ seal support system the ideal solution?
The split system allows you to be certain in the case of a seal failure that the system is clean. On any pump seal replacement the last thing you need is for a dirty barrier fluid system to be the cause of the next or early seal failure.
Was the company pleased with the result and have they placed further orders?
Yes, and the standard upgrade for this site is now the DMSF and EasyClean™. Also this is now the specification on new pumps and replacement of older units. The upgrade to historic equipment shows how the results met and exceeded expected results.
Related Case Studies