Case Ref
CS0041
Country
United Kingdom
Summary
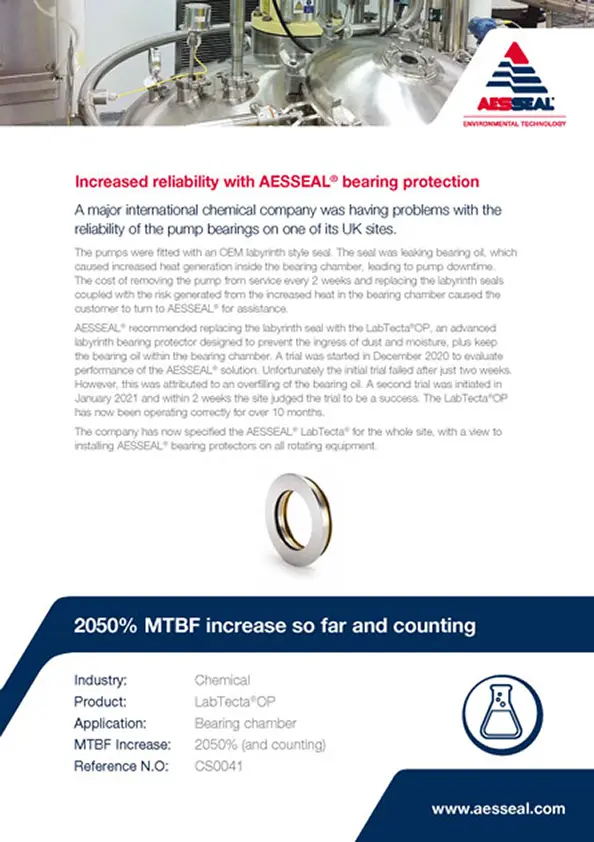
A major international chemical company was having problems with the reliability of the pump bearings on one of its UK sites.
More Industry Related Content
Related Products Pages
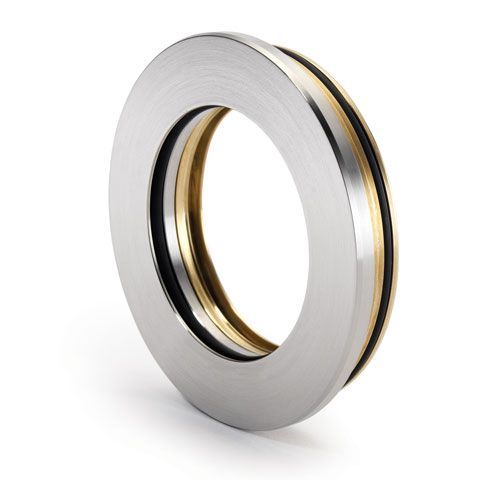
Cost effective pump bearing protection upgrade solution
Related Case Studies
Reliable solution for high pressure, high temperature agitator application
Specialty Chemical Company achieves improved reliability
Chemical company saves £9,400 and 17,000m3 of water a year
Polish plant benefits from LabTecta protection
Chemical plant saved over €500,000 in the first year
AESSEAL product eliminates serious health hazard
Gas seal gives 14 years trouble free operation
Reliability upgrade improves Mean Time Between Failure by 5 times