Case Ref
CH01166
Country
Australia
Summary
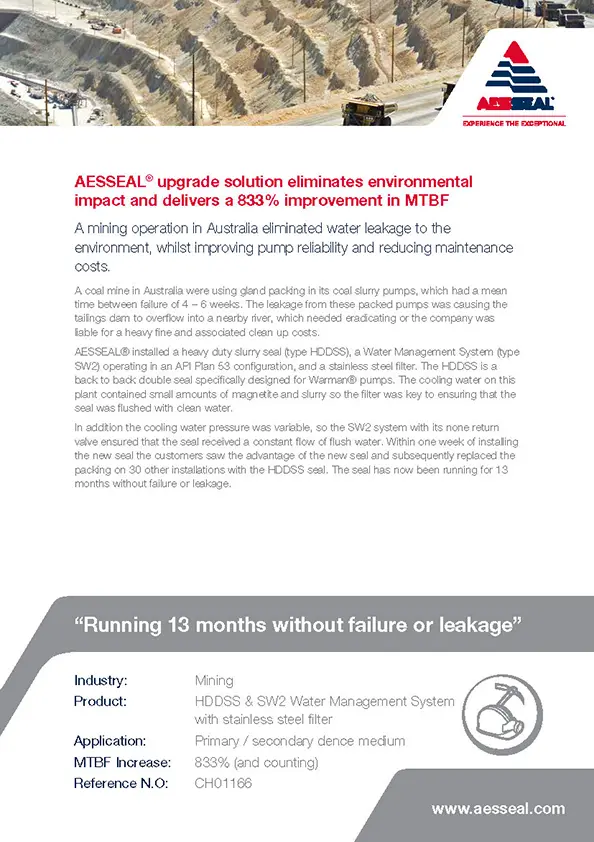
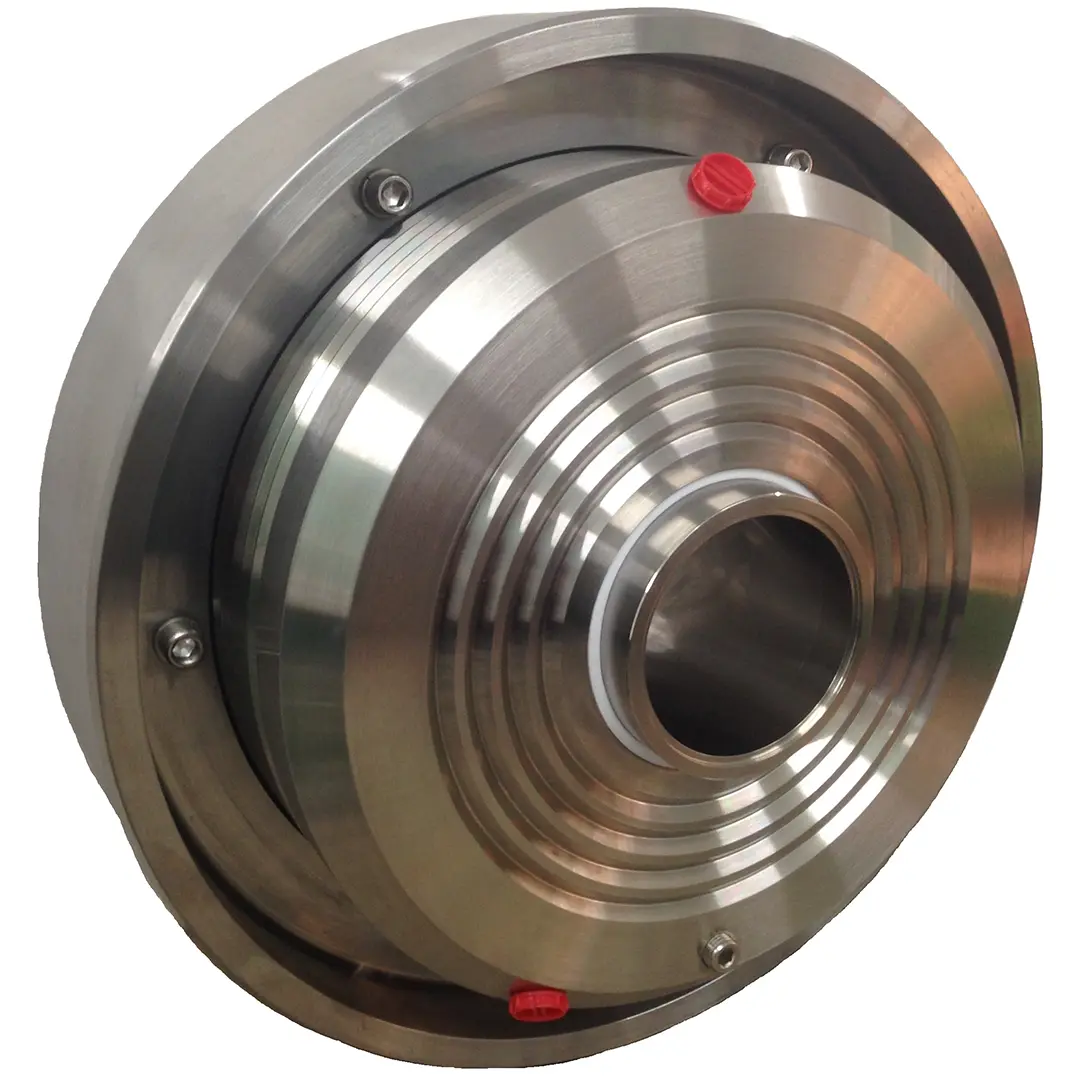
A mining operation in Australia eliminated water leakage to the environment, whilst improving pump reliability and reducing maintenance costs.
More Industry Related Content
Environmental Social Corporate Governance
Related Case Studies
AVT sensors save thousands for US company
Mining company saves $8 million AUD with AESSEAL system
Mechanical Seal upgrade improve reliability and saves more than ZAR 580,000
HDDSS brings savings for Australian mining company

Major savings for SA company
Replacing gland packing reduces cost, and improves reliability
LabTecta FS the answer for gearbox problem
HDDSS seal ensures safer workplace at Australian plant