Case Ref
CH00886 - CH00897
Country
United Kingdom
Summary
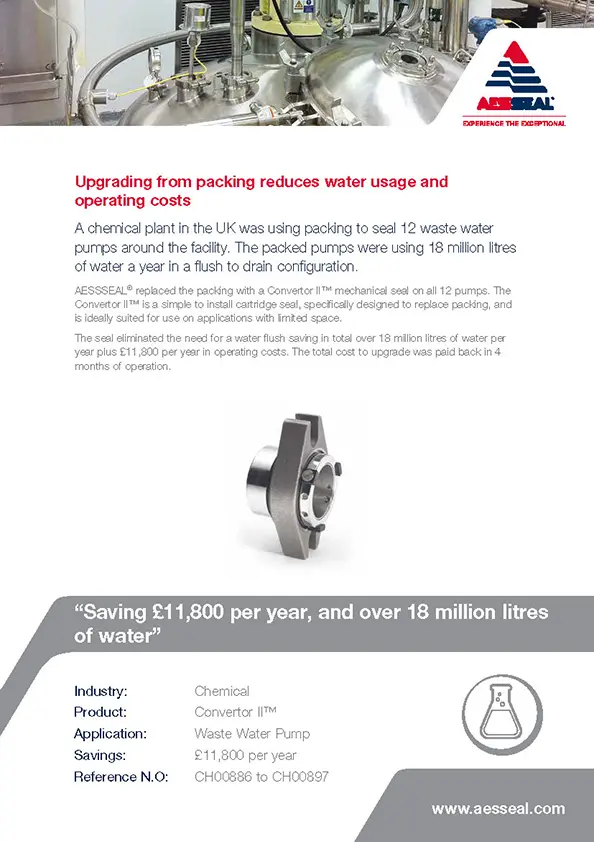
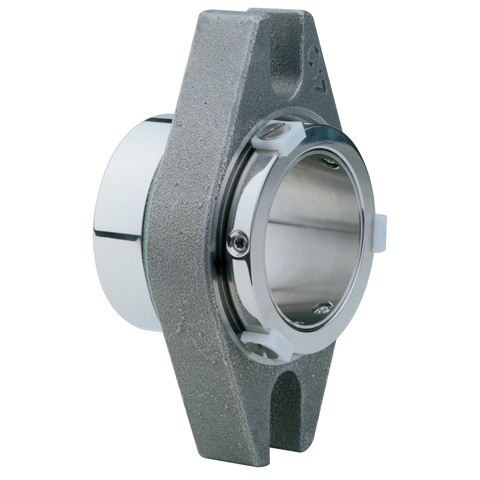
A chemical plant in the UK was using packing to seal 12 waste water pumps around the facility. The packed pumps were using 18 million litres of water a year in a flush to drain configuration.
More Industry Related Content
Environmental Social Corporate Governance
Related Case Studies
Reliable solution for high pressure, high temperature agitator application
Chemical company saves £9,400 and 17,000m3 of water a year
Upgrade delivers annual saving of 15,000 USD
AESSEAL mixer seal solves reliability problem
CAPI™ boosts reliability at South African plant
Specialty Chemical Company achieves improved reliability
DMSF seals halt water leakage
Efficient seal support system reduces energy costs