Case Ref
CH03469
Country
United Kingdom
Summary
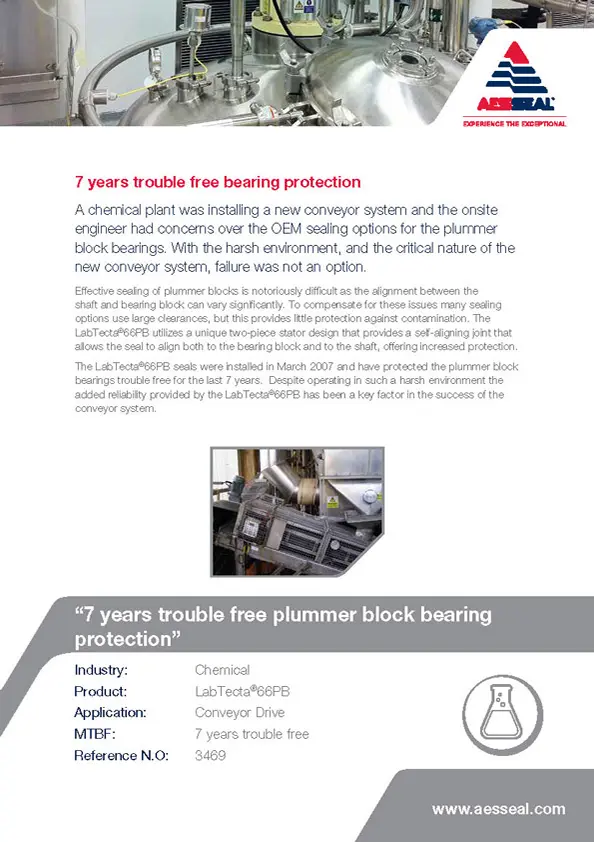
A chemical plant was installing a new conveyor system and the onsite engineer had concerns over the OEM sealing options for the plummer block bearings.
More Industry Related Content
Related Products Pages
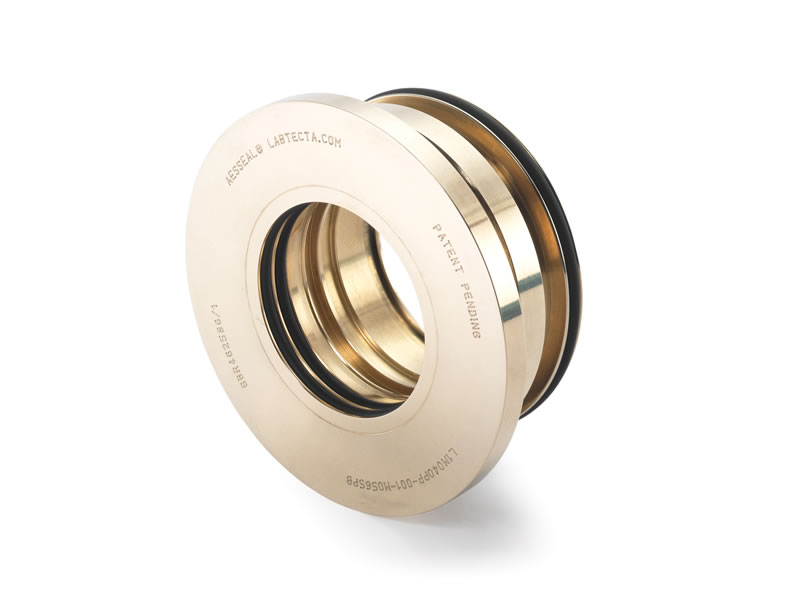
Plummer/Pillow Block Bearing Protection
Related Case Studies
Specialty Chemical Company achieves improved reliability
Quality of service key to AESSEAL contract
AESSEAL upgrade solution improves MTBF and reduces costs
Chemical company saves over $225,000 in first year
LabTecta delivers reliability improvement
Saving water, the environment and our customers money
Chemical Producer Saves Over £1.7 Million in Plant Downtime
Reduced downtime, improved safety