Featured Case Studies
The case studies below showcase the very best of commitment to excellence at AESSEAL across our three core pillars:
- Exceptional Customer Service – putting customers first, every time.
- Advanced Technology – delivering innovation that drives results.
- Sustainable Solutions – engineering a better future for people and our planet.
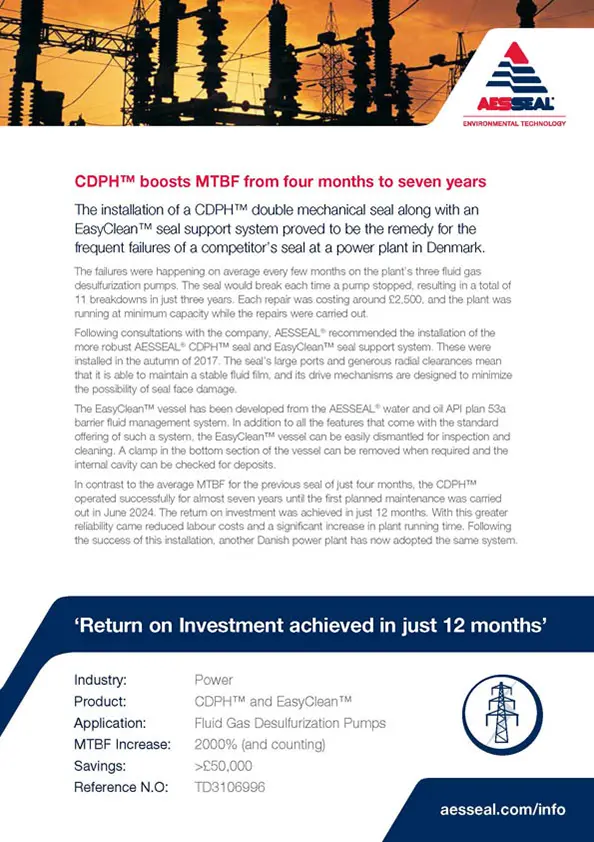
CDPH & EasyClean boosts MTBF from four months to seven years

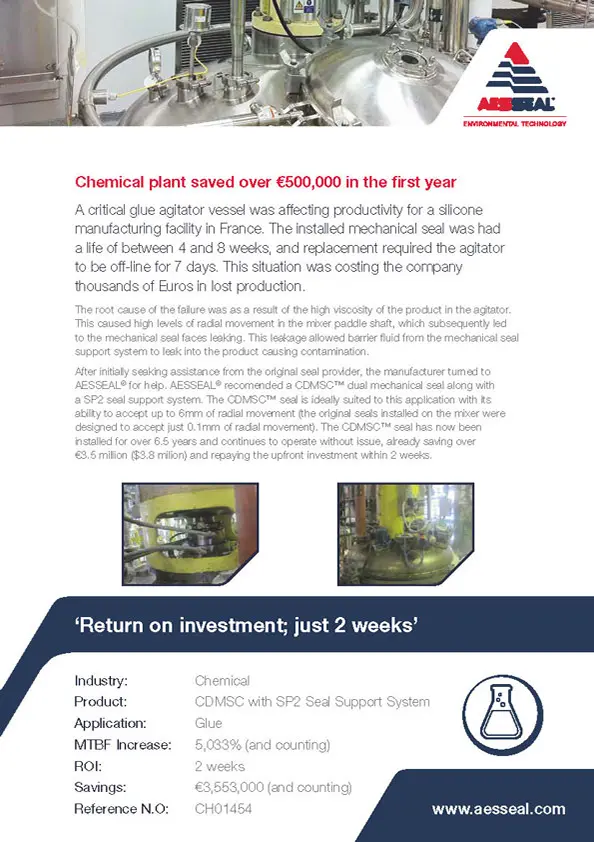
Chemical plant saved over €500,000 in the first year

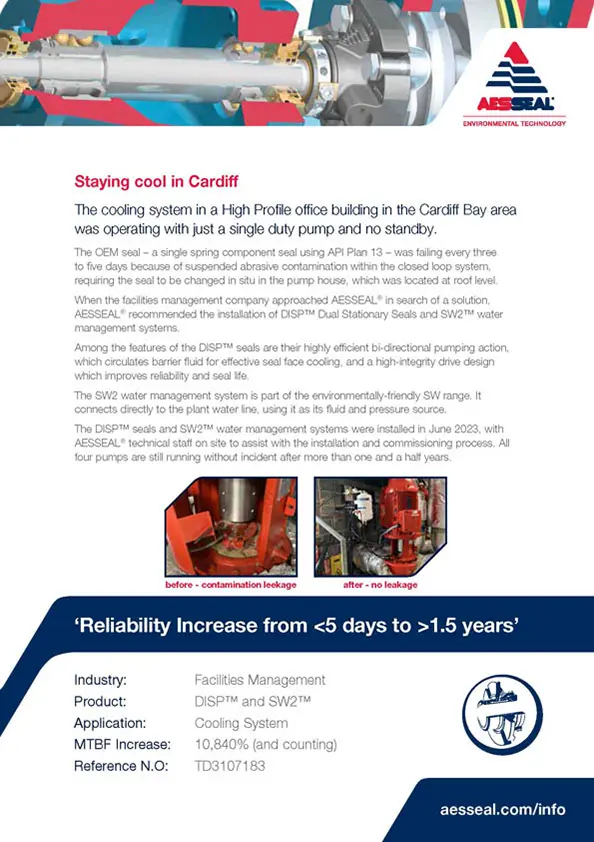
Staying cool in Cardiff

Annual savings of over $2.6 million

CURC seal saves thousands for US company
DMSF makes its mark in Japanese paper industry

80 million litres of water per year to be saved at Mexican mine

Upgrade will result in major savings for US company
AESSEAL packing system brings major savings
A French pharmaceuticals company has saved over €200,000 in the first year following its decision to change to an AESSEAL reactor packing system.
FIDC ends costly leaks at US firm
Change to packing saves Swiss company $millions

A chocolate producer in Switzerland has saved around ₣2.3 million ($2.6 million) over the past year following its decision to change to an AESSEAL pump packing system.
Bitumen pump upgrade saves over £23,000 a year
Asphalt producer pump for road surfaces was gland packed and losing over 15 tonnes of bitumen.
LabTecta ends dust pollution problem for SA firm

Preventing dust from escaping into the working environment and is saving thousands of dollars a year
AESSEAL product brings big savings for South African company
AESSEAL solves reliability problem for US paper company
LabTecta FS the answer for gearbox problem

Major savings follow installation of TPDS™ slurry seal

ASSEAL's TPDS heavy duty mechanical seal saves an Australian mining company an estimated AU$240,000 (US$168,000) over three years.
Mechanical seals runs an incredible 17 years without problems
AESSEAL product stops hot oil pump leakage

CFFC™ solves reliability problem on North Sea oil platform
ROI In Less Than A Month
LabTecta ends contamination problem at Australian mining company
Warman conversion the answer for Spanish company

A seal conversion kit for the Warman® AH Range of Ultra Heavy Duty Slurry Pumps helped to solve a variety of problems being experienced by a Spanish aluminium producer.
Major savings follow installation of AESSEAL product

A petrochemical company based in the Middle East was having problems with persistent and costly seal failures.
AESSEAL product removes risk of HFC emissions

AESSEAL system fixes sewage problems for US township
A municipality in Pennsylvania was having issues with major inefficiencies in its sewage treatment system.
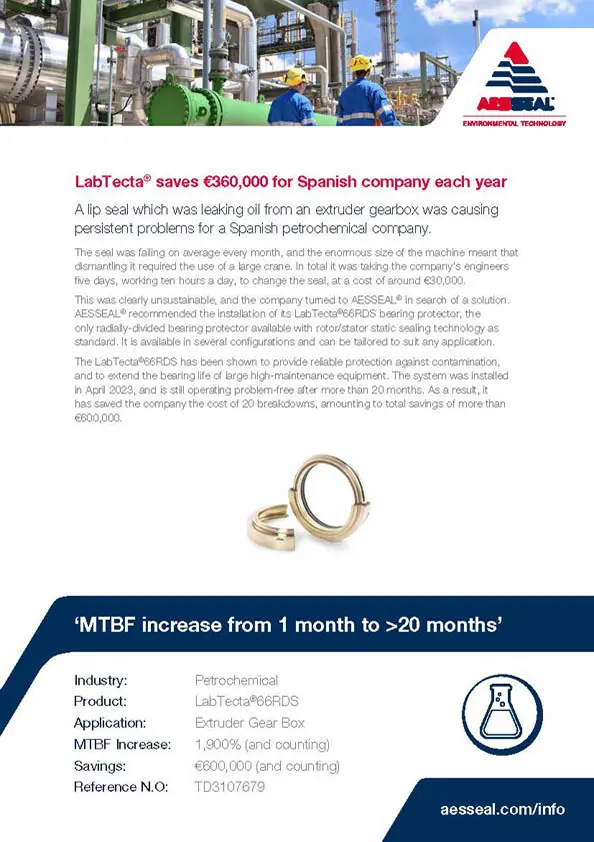
LabTecta saves €360,000 for Spanish company each year
DMSF solves reliability issues for Swedish company

AESSEAL helps UK firm to multi-million pound savings
CDSA seals brings huge savings for US company
Rapid response saves the day for UK company
Mining company saves $8 million AUD with AESSEAL system
New approach for slurry pumps reduces water usage by 95%

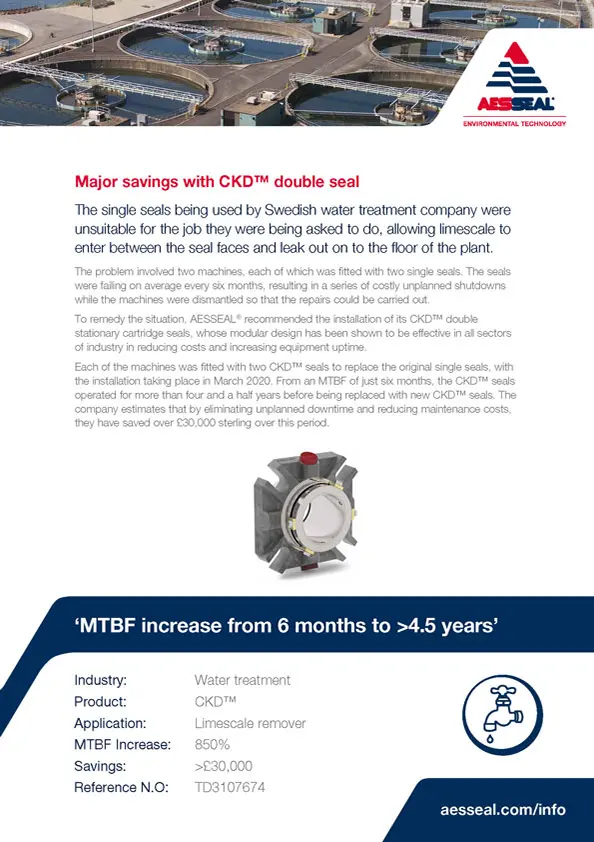
Major savings with CKD double seal
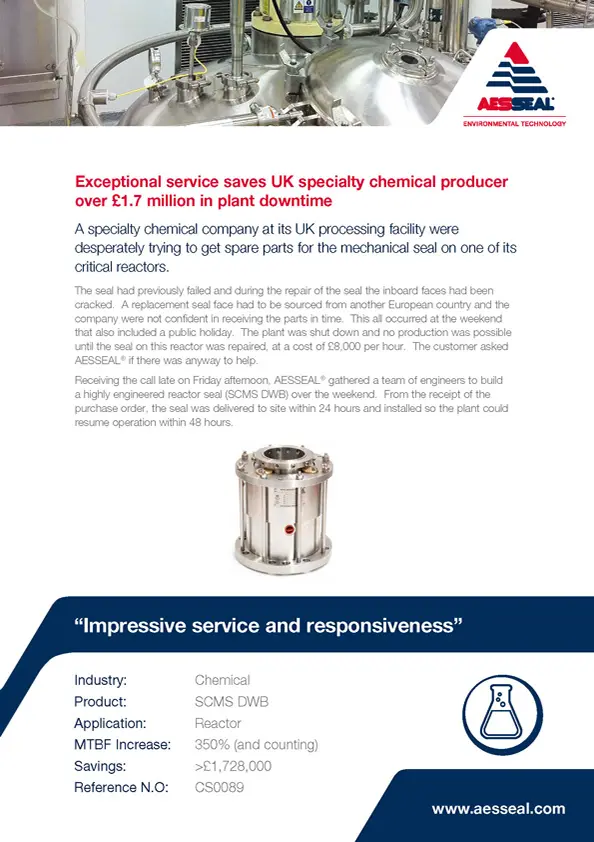
Chemical Producer Saves Over £1.7 Million in Plant Downtime
Exceptional service saves thousands in lost revenue
AESSEAL were contacted by a power plant in the UK who were experiencing a major issue with their supply of mechanical seals.

AESSEAL raises spirits at UK distillery
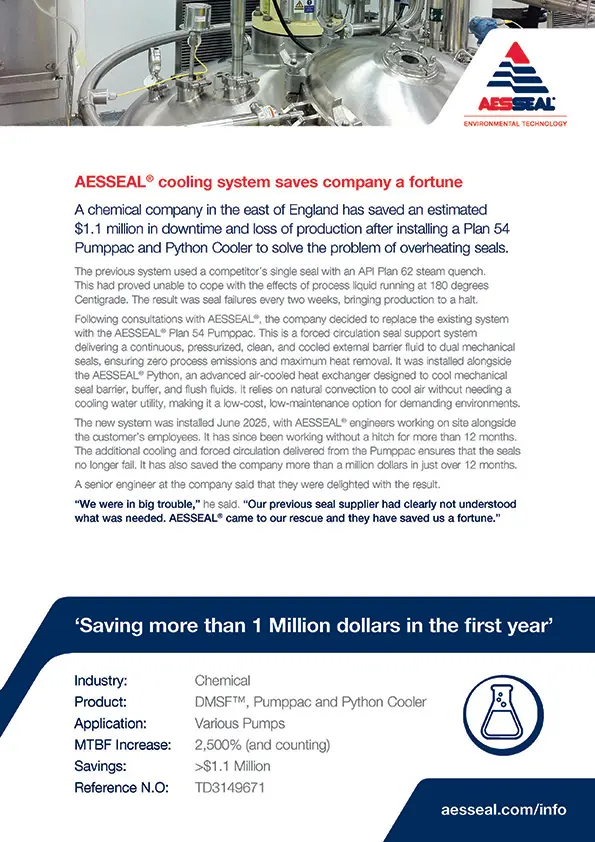
AESSEAL cooling system saves company a fortune
Rapid response impresses Saudi customer

Sourced and supplied a replacement seal in just two weeks for customer’s Oil and Gas operation in Saudi Arabi
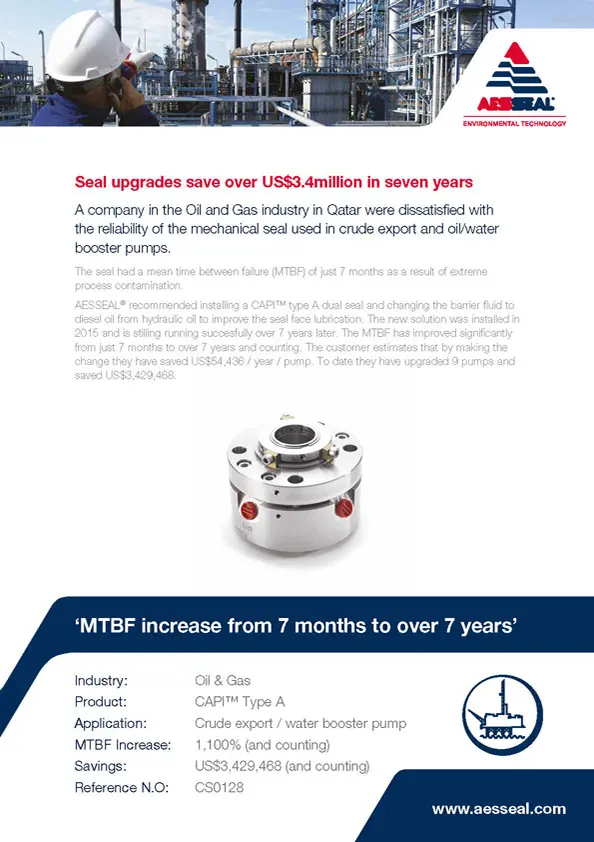
Seal upgrades save over US $3.4million in seven years

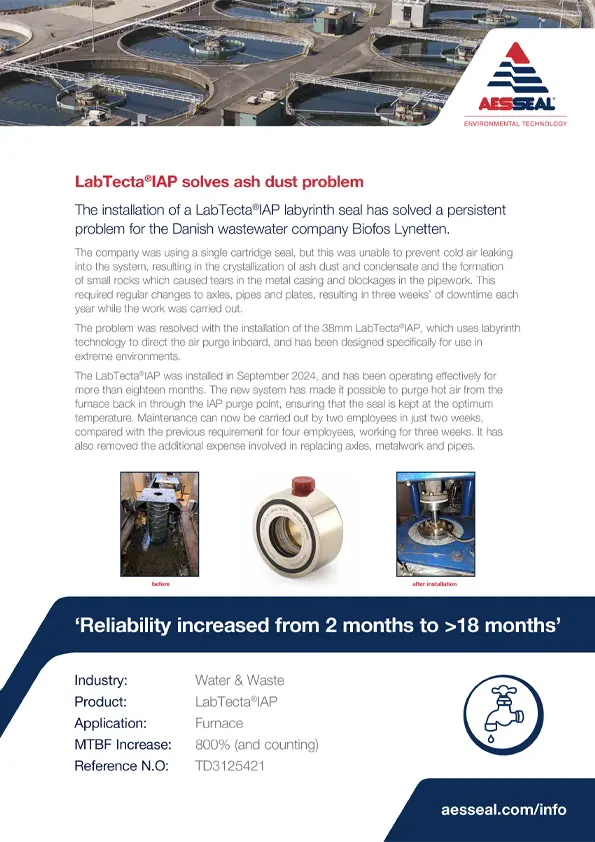
LabTecta IAP solves ash dust problem
Counterproductive flush water in an evaporator pump leads to big savings

During an energy audit at a Canadian pulp and paper plant, AESSEAL identified 15 packed evaporator area pumps that needed upgrading to mechanical seals.
Improving reliability, increasing efficiency